
Die and mold manufacturing
Operation: Cavity blending, radii finishing, slot cleanup and edge breaking
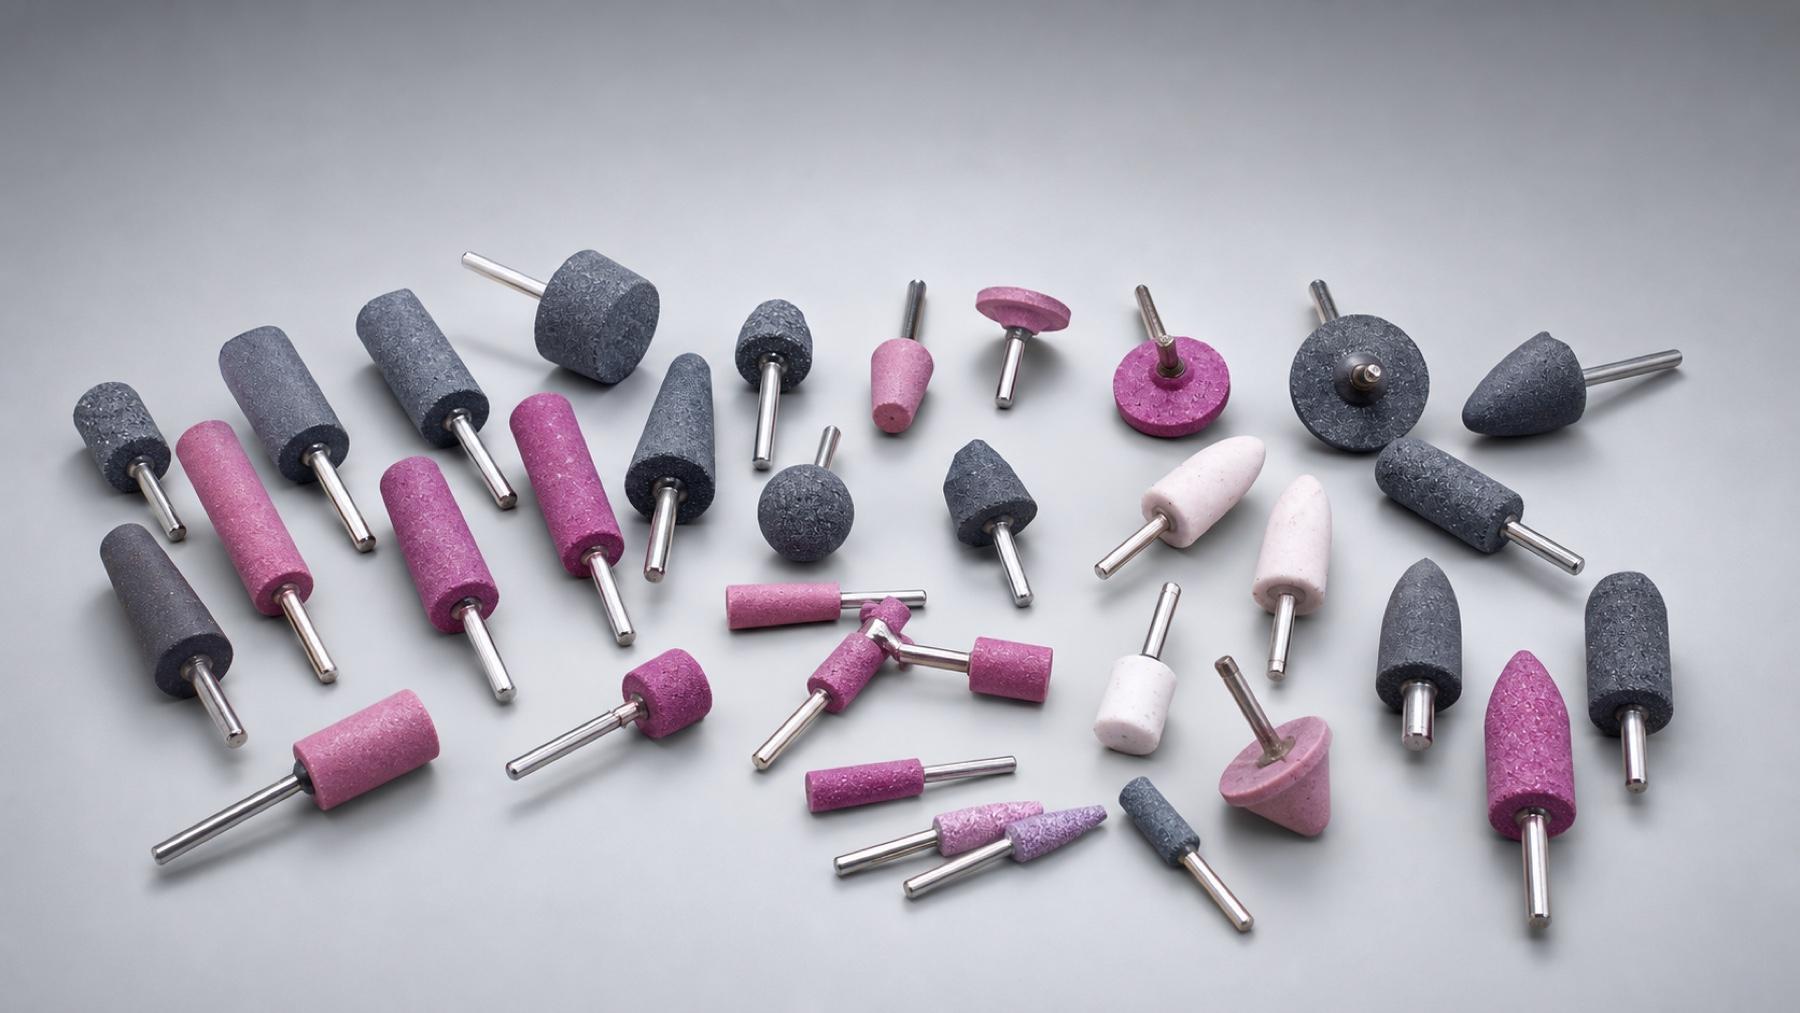
Typical products: Cone, round-nose and cylindrical mounted points
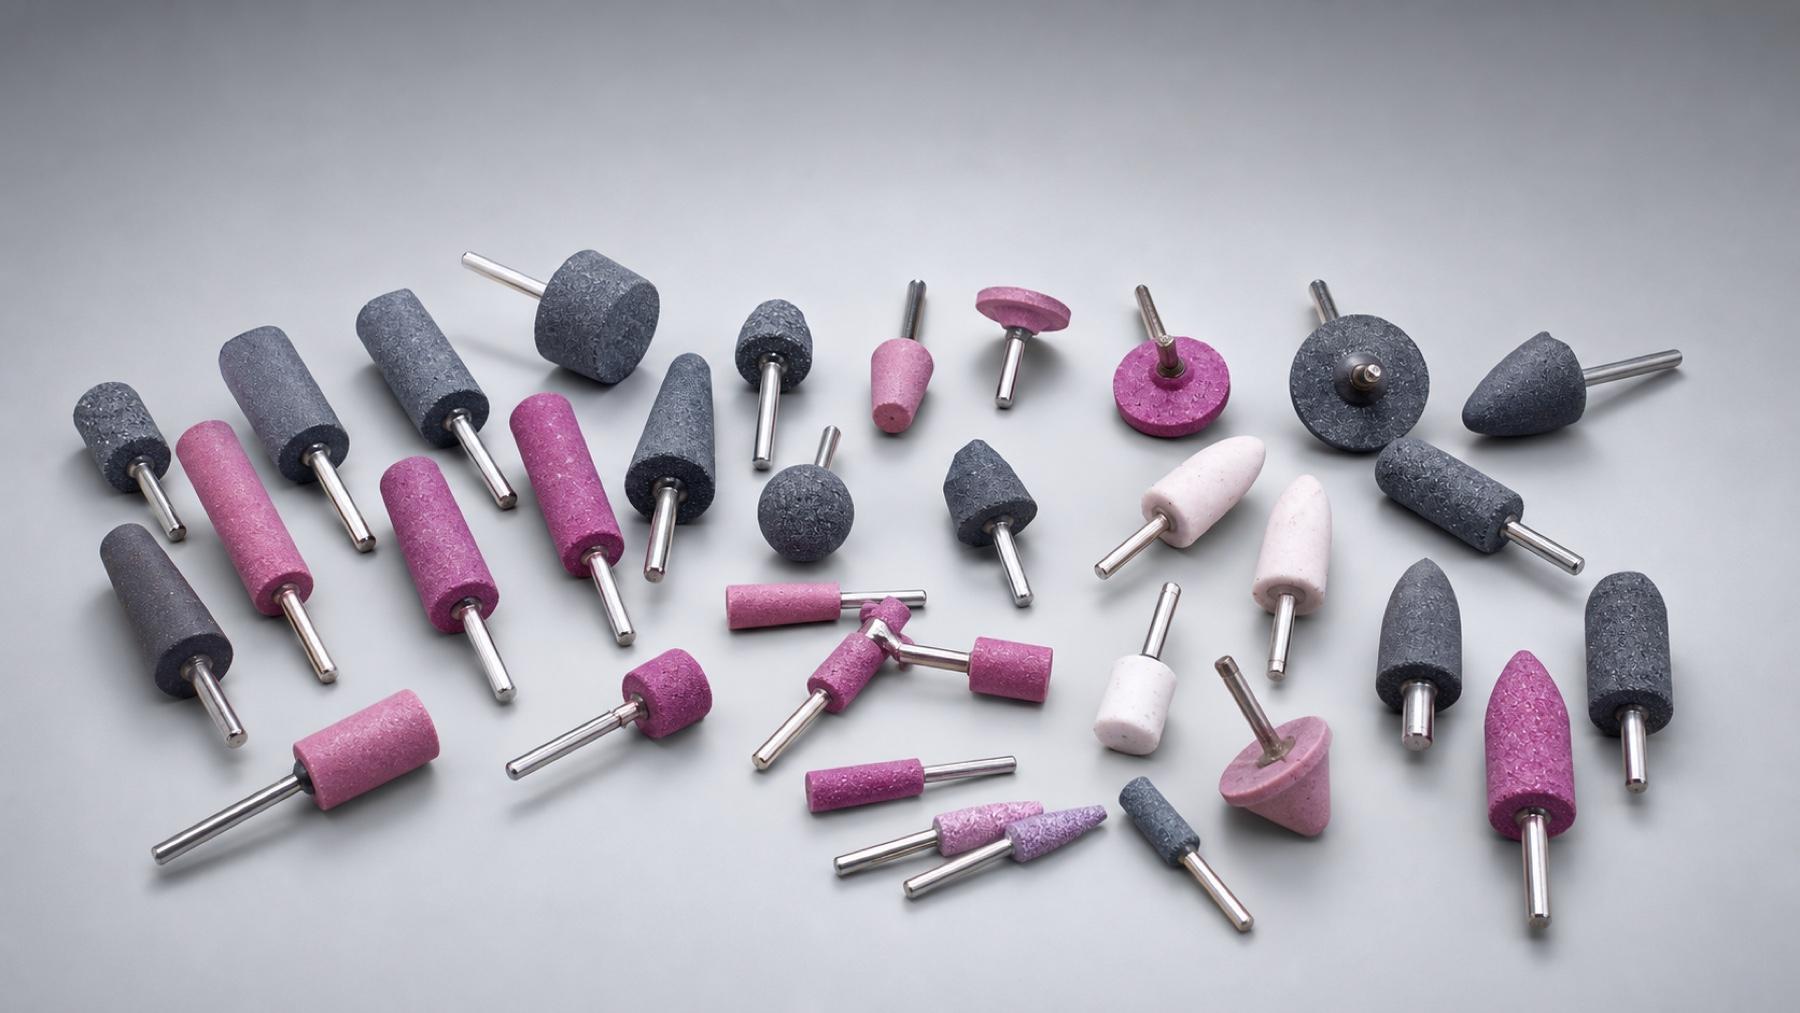
Industrial RFQ brochure
Mounted Points and Custom Abrasive References
A practical buyer brochure for bonded abrasive mounted points, oil stone and abrasive stick RFQs, custom abrasive specifications and repeat industrial enquiry support.
Works Address
124, New Shiv Puri, Behind J.P. Public School, Aara Mill, Khurja - 203131, Uttar Pradesh, India
GST
09APXPM7548B1ZA
Document
Industrial catalogue / RFQ edition
Contact
info@sadhviudyog.com
+91 87916 94259
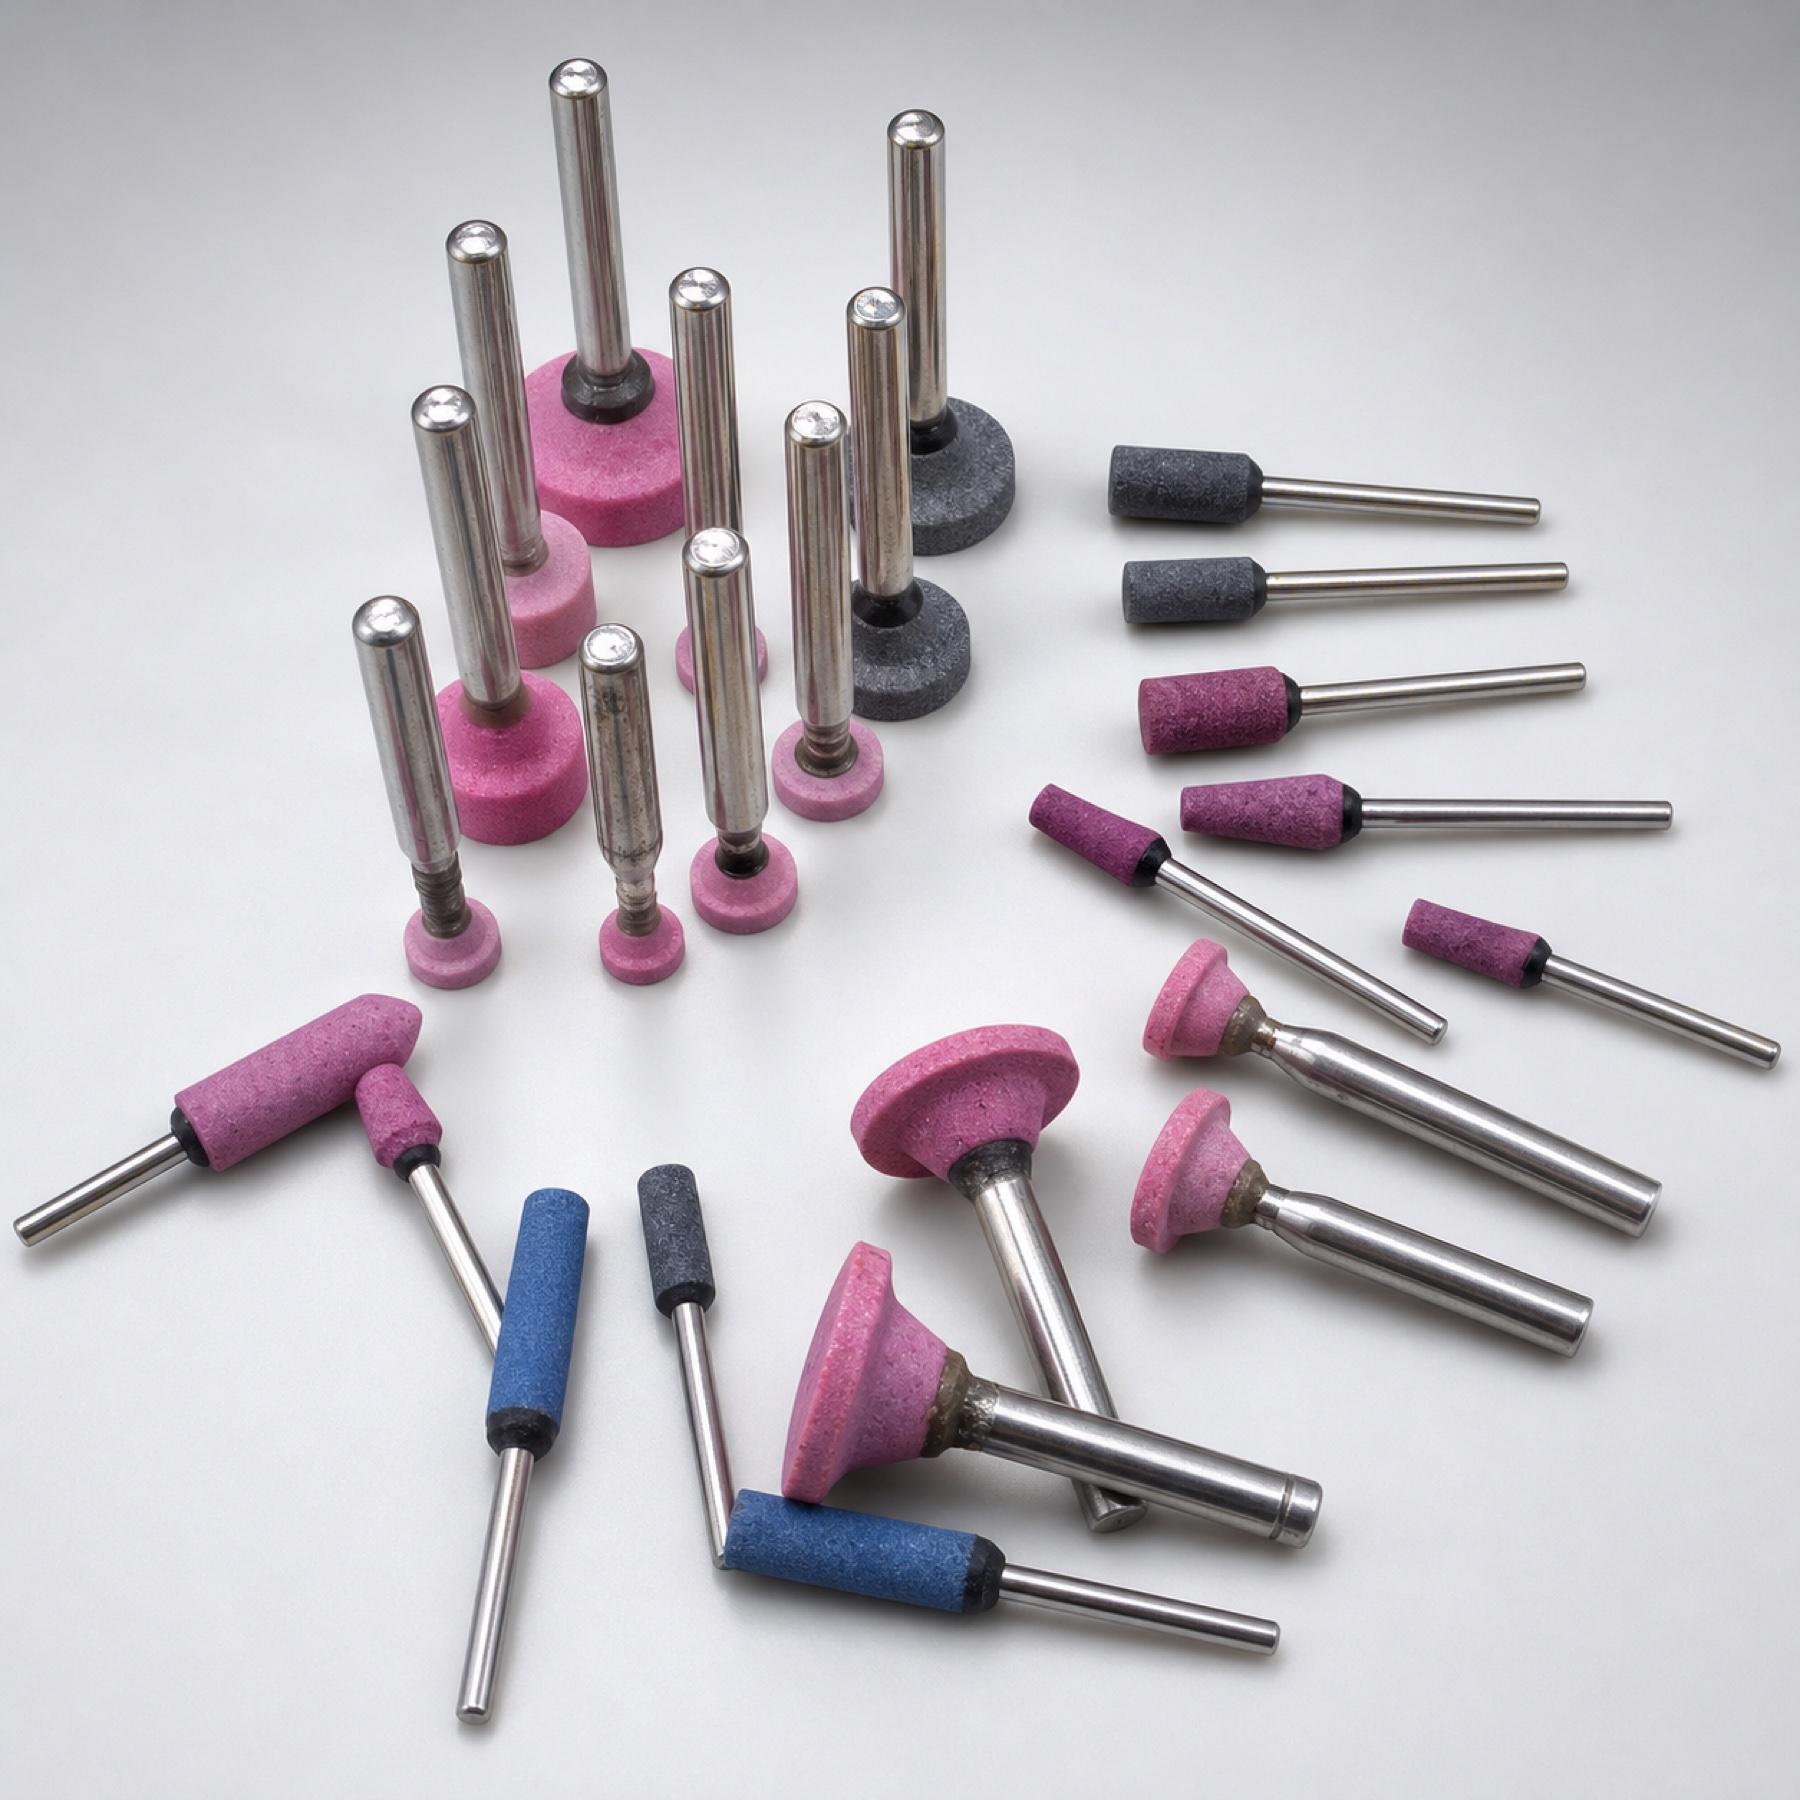
A / W / B
Cylinder, cone, bullet, round-nose and small-shank forms for die grinder work.
A / WA / PA / C
Aluminum oxide, white aluminum oxide, pink aluminum oxide and silicon carbide options.
Vitrified bond
Porous bonded abrasive structure for form retention and controlled stock removal.
Custom RFQ
Non-standard shapes, grit mixes, hardness and shank dimensions quoted on request.
Catalogue index
Brochure purpose
This brochure is built to help purchase teams, production engineers and maintenance shops discuss abrasive requirements clearly with Sadhvi Udyog. It explains what the company supplies, how product families fit common grinding work, and which details are needed before quotation.
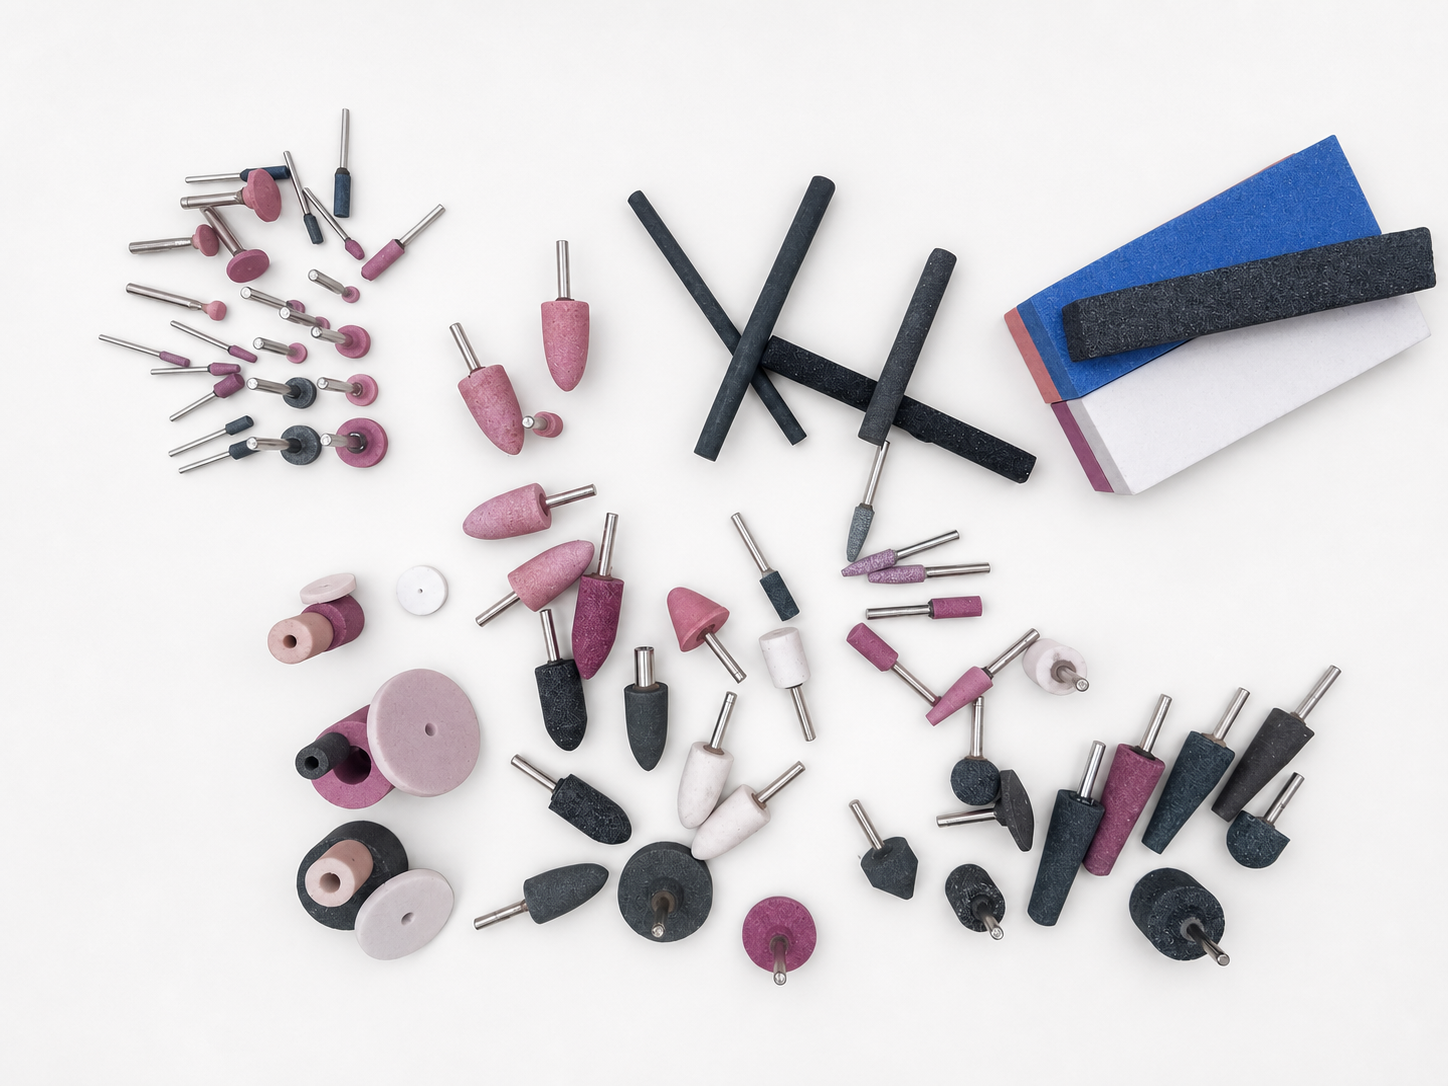
Vitrified mounted points are the primary manufactured range, supported by oil-stone, abrasive-stick and custom abrasive RFQ references.
Start with the application, shortlist the product family, then confirm shape, size, grain, grit, bond, speed marking and quantity before quotation.
Share the required profile, drawing or sample with machine RPM, work material, operation, trial quantity and packing expectation for a clearer RFQ.
Company profile
Sadhvi Udyog manufactures and supplies vitrified mounted points. Oil stone, abrasive stick and custom abrasive entries are RFQ references for buyers who need to confirm shape, grit, bond, speed marking and quantity before ordering.
Identity: Manufacturer and supplier of abrasive mounted points, oil stones, abrasive sticks and custom abrasive tools quoted on request
Address: 124, New Shiv Puri, Behind J.P. Public School, Aara Mill, Khurja - 203131, Uttar Pradesh, India
GST: 09APXPM7548B1ZA
Small bonded abrasive tools for die grinders, flexible shafts and precision hand-held grinding.
Non-standard sizes, grains, grades and packing can be discussed against material, machine and quantity.
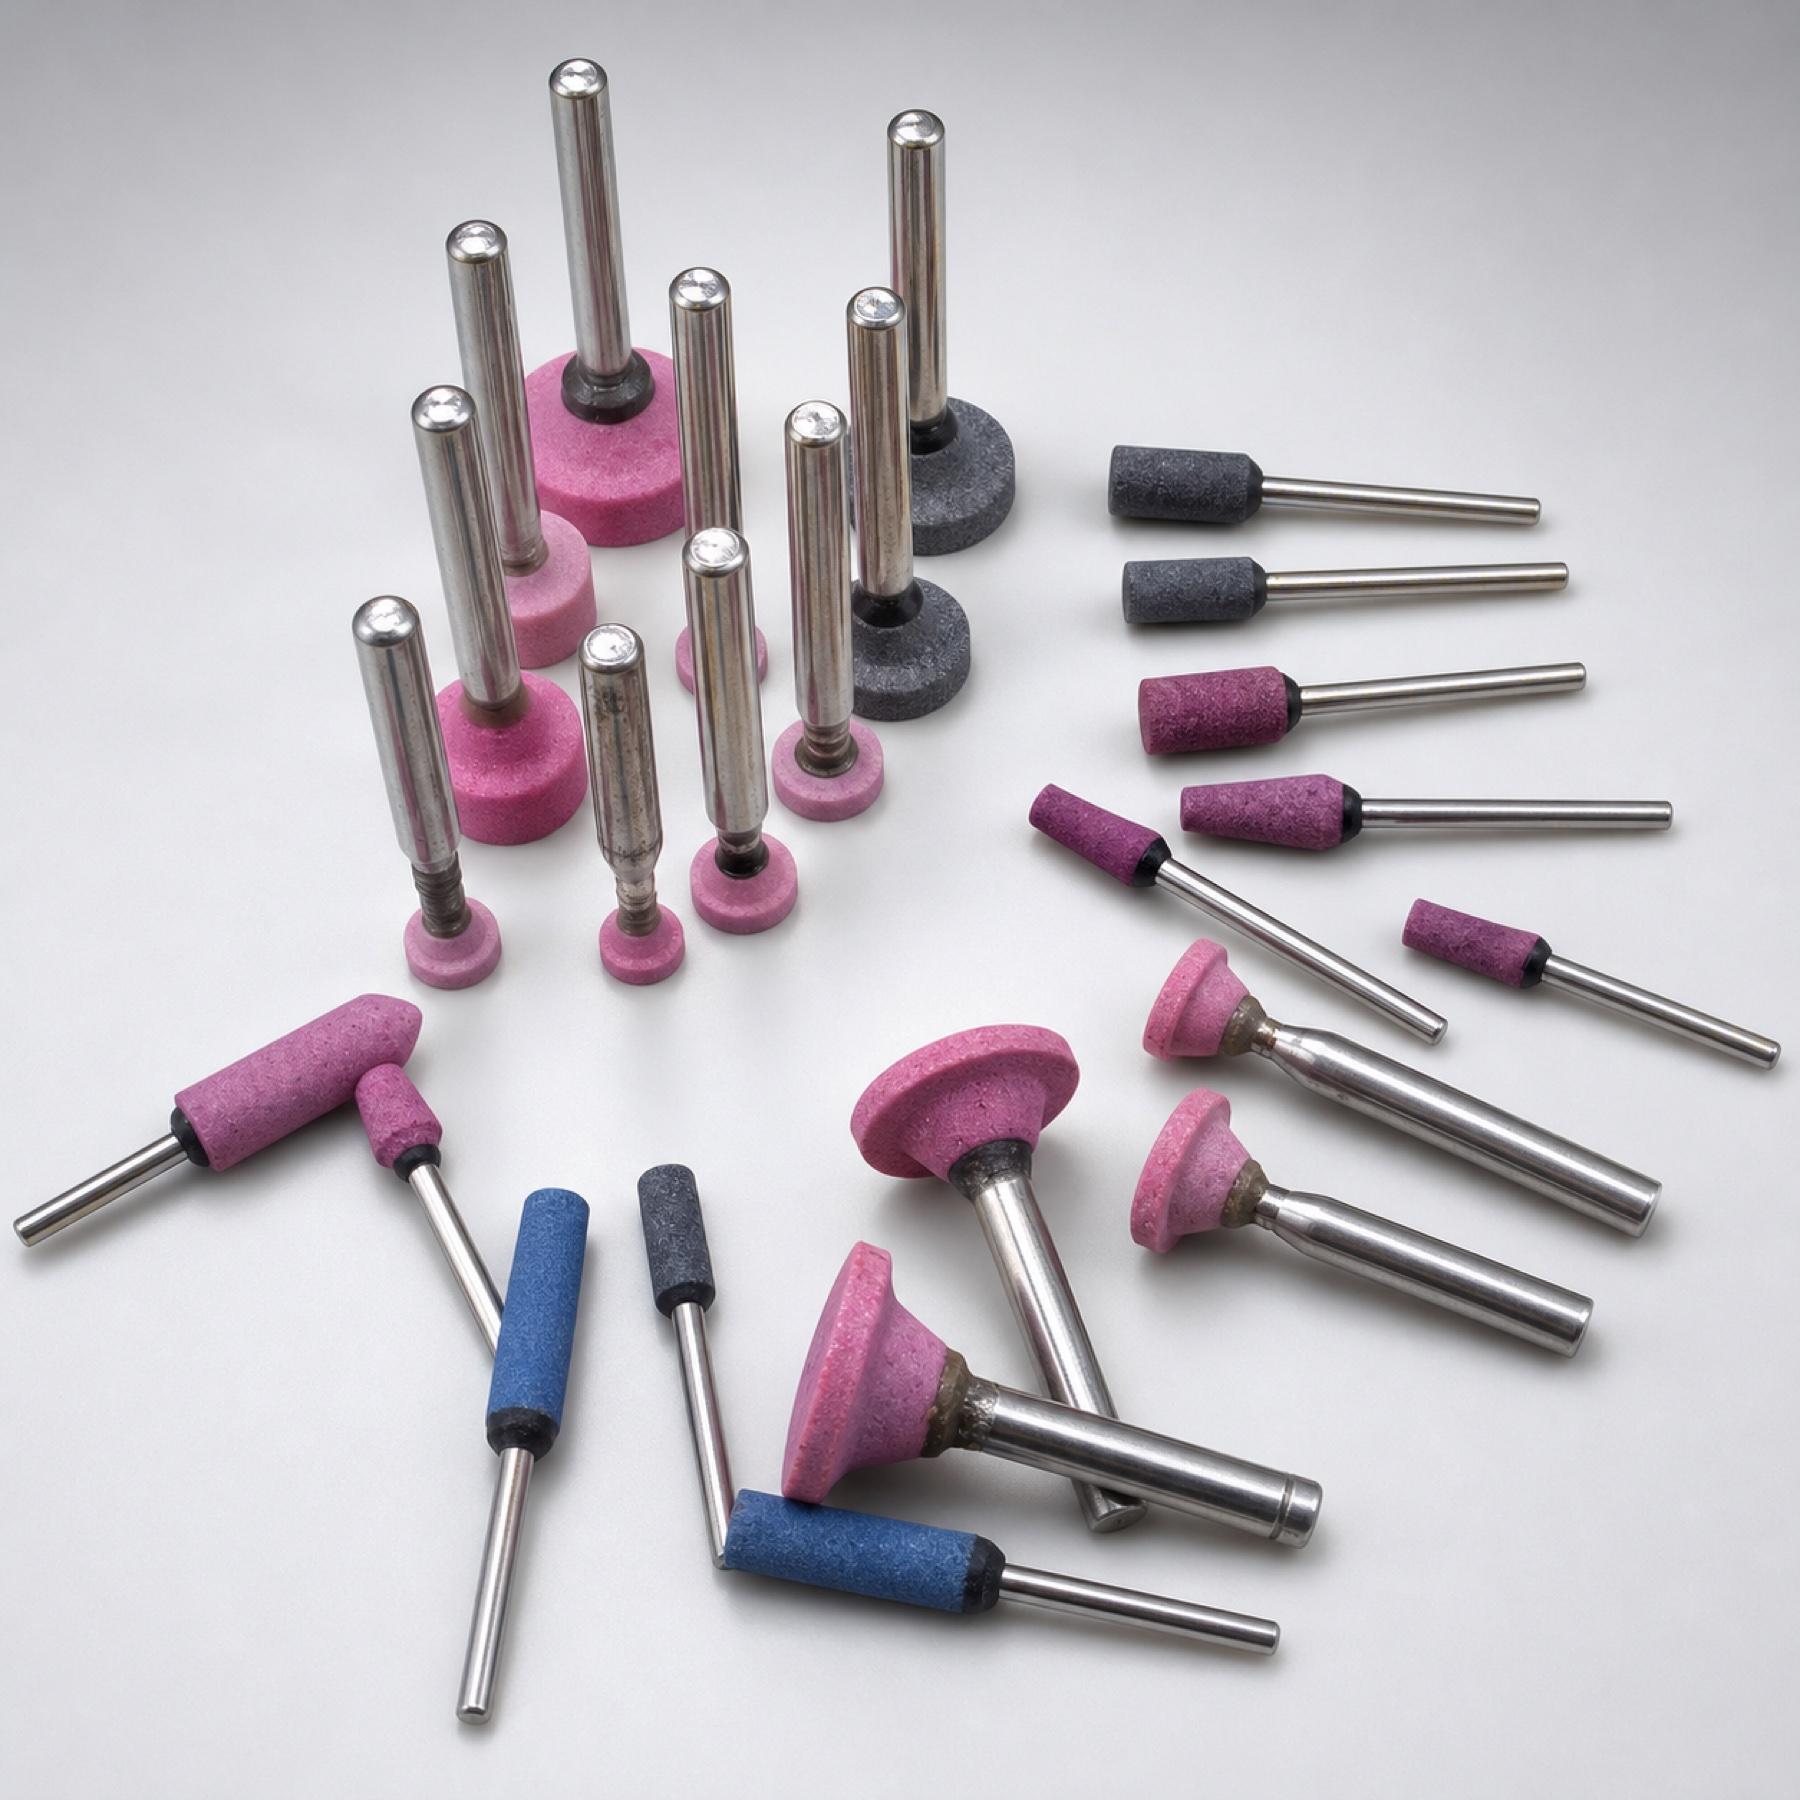
Range at a glance
12
online profile references
Custom
abrasive RFQs supported
3 mm / 6 mm
common mounted-point shanks
24-320
typical grit coverage
Work material, machine speed, operation, profile, body size, shank size, abrasive grain, grit, grade, bond and monthly consumption.
Shape and profile range
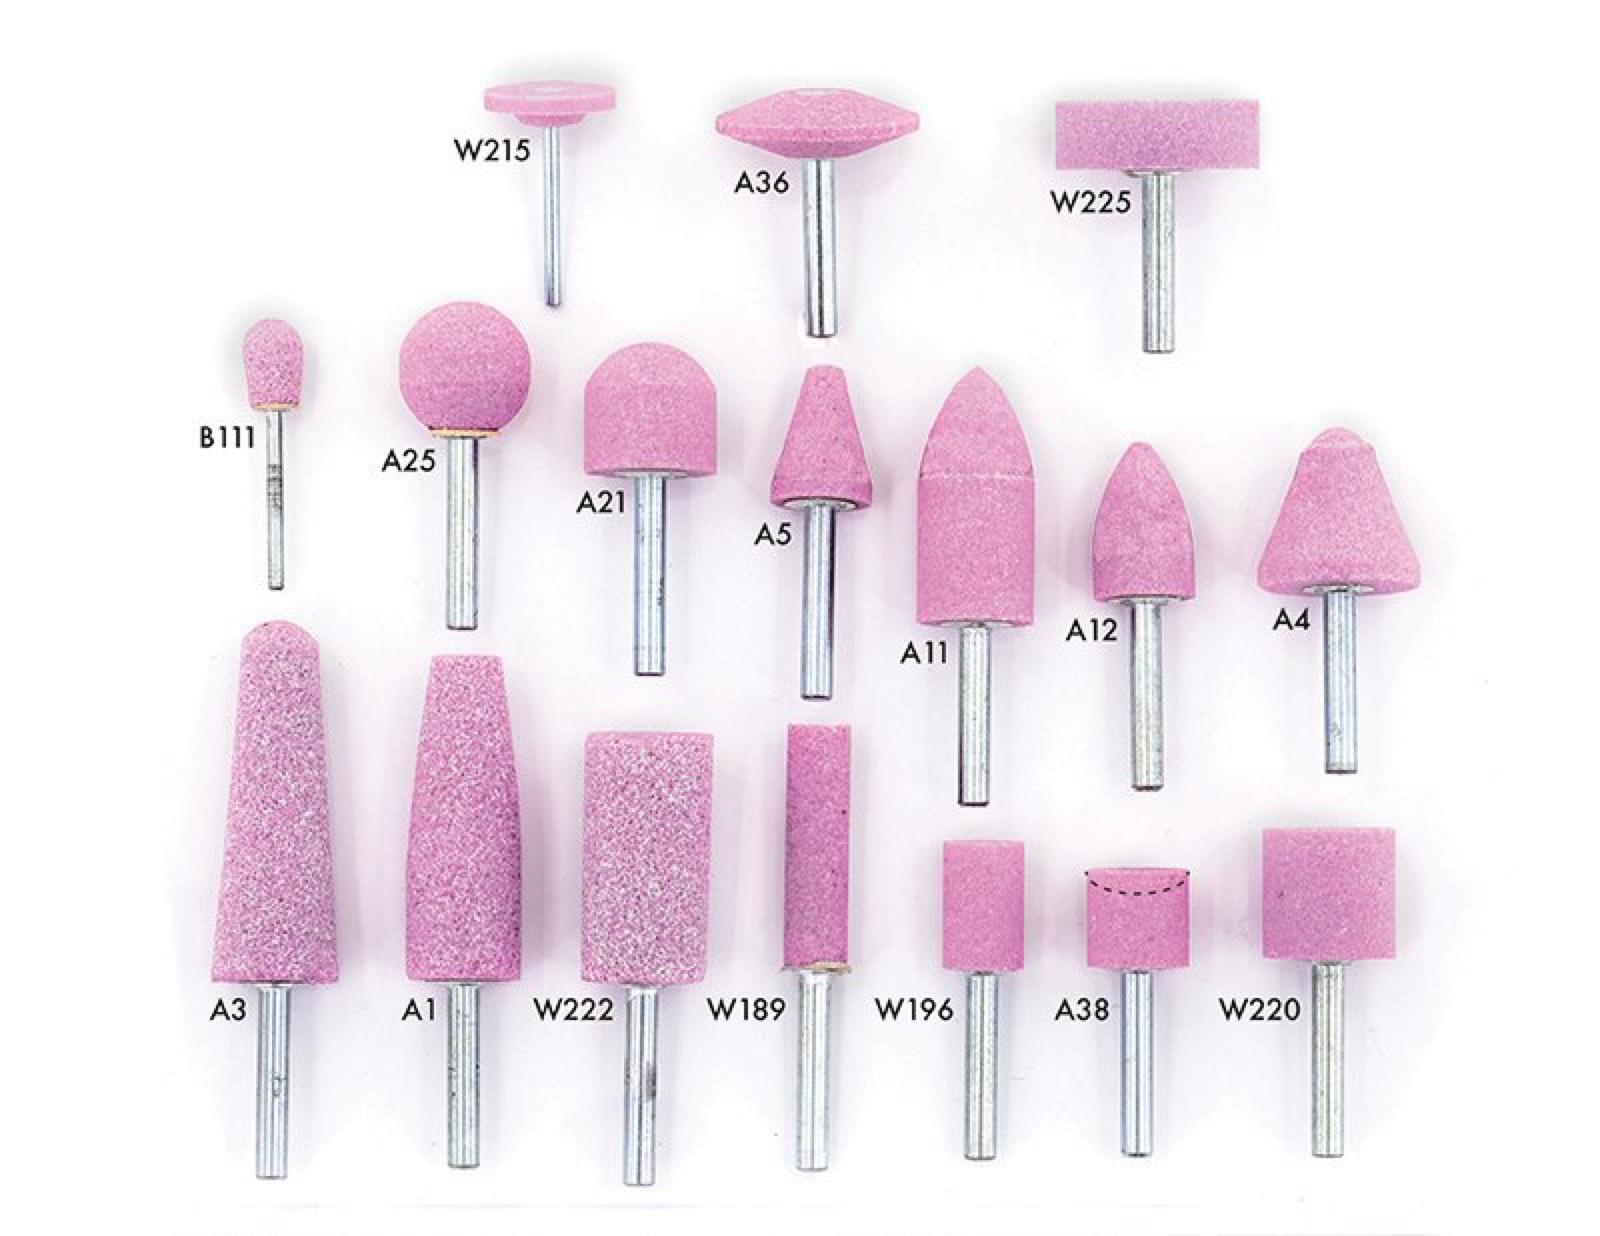
These price-free charts are taken from a business-supplied customer reference. They show shape variety and nominal dimensions only. Final availability, specification, packing and commercial terms are confirmed through a quotation.
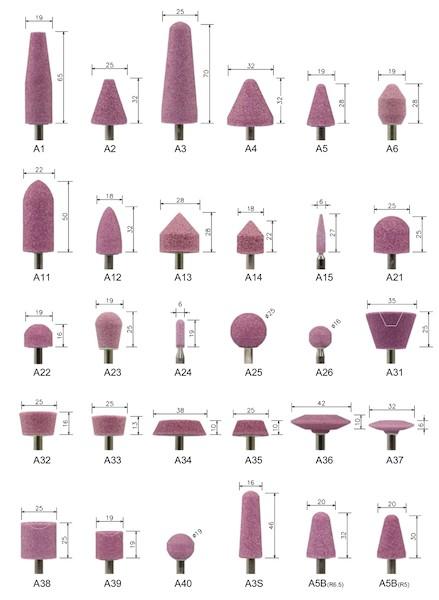
A broad profile family covering tapered, pointed, rounded, ball, wheel, cup and cylindrical forms.
Use the chart to identify shape only; dimensions and availability require RFQ confirmation.
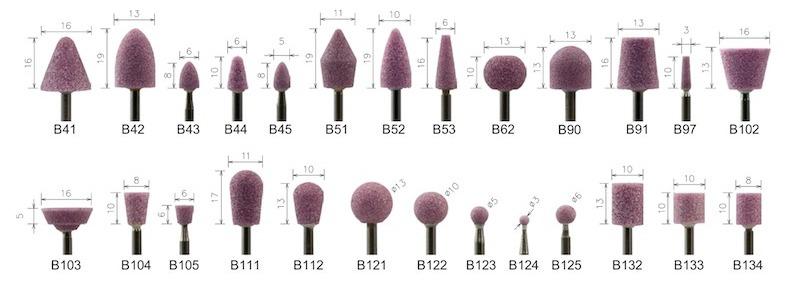
Compact spindle-mounted forms for restricted access, detail grinding and small-area finishing.
The source chart includes nominal dimensions; confirm spindle, body size and machine fit before ordering.
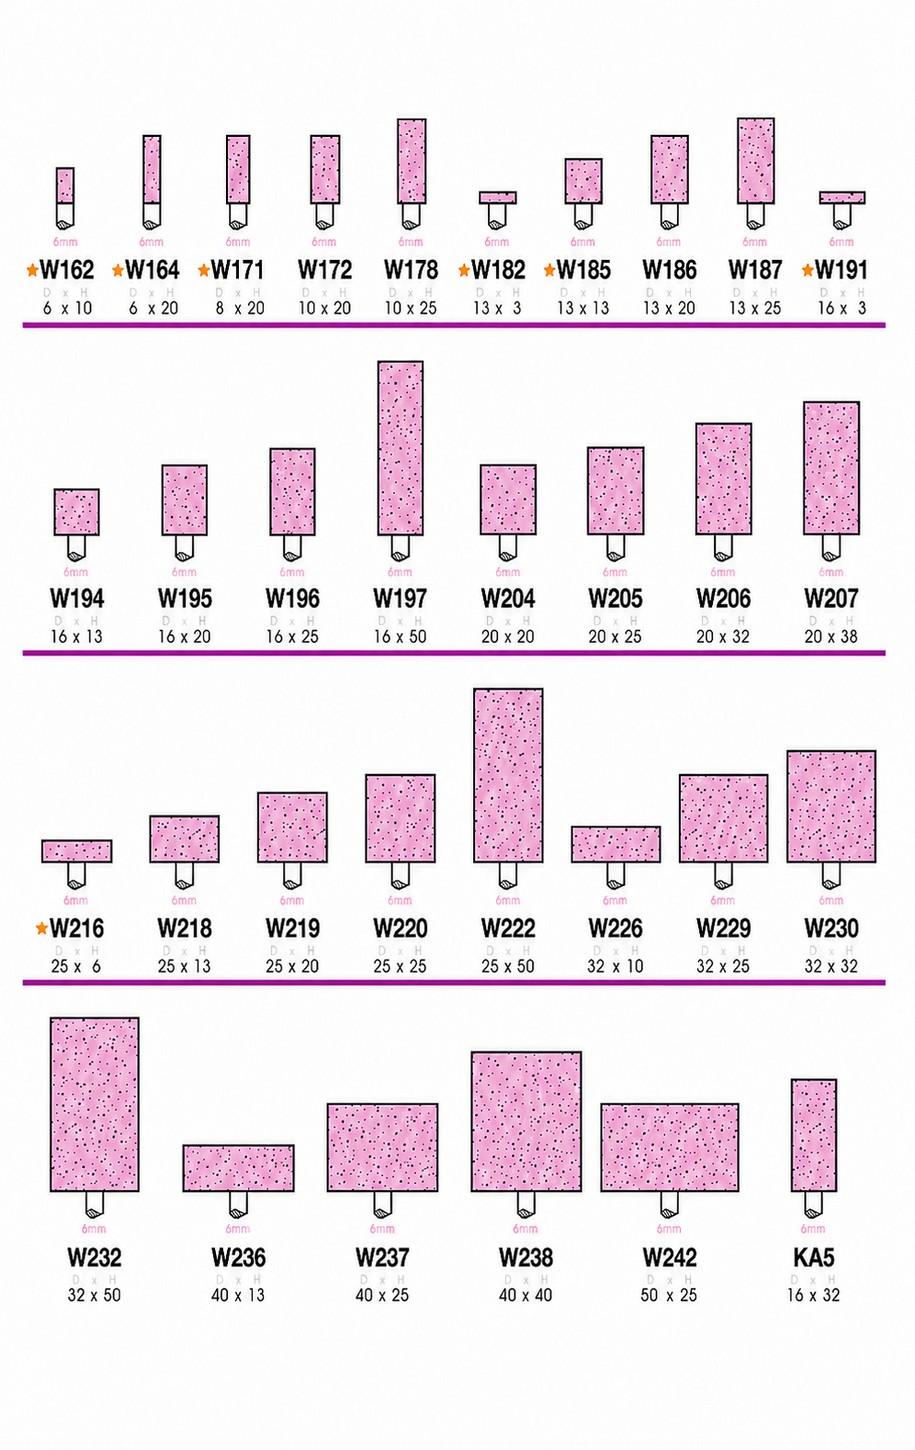
Cylindrical and wheel-form references ranging from compact bodies to larger grinding faces.
Codes and dimensions are identification references, not confirmation of current stock.
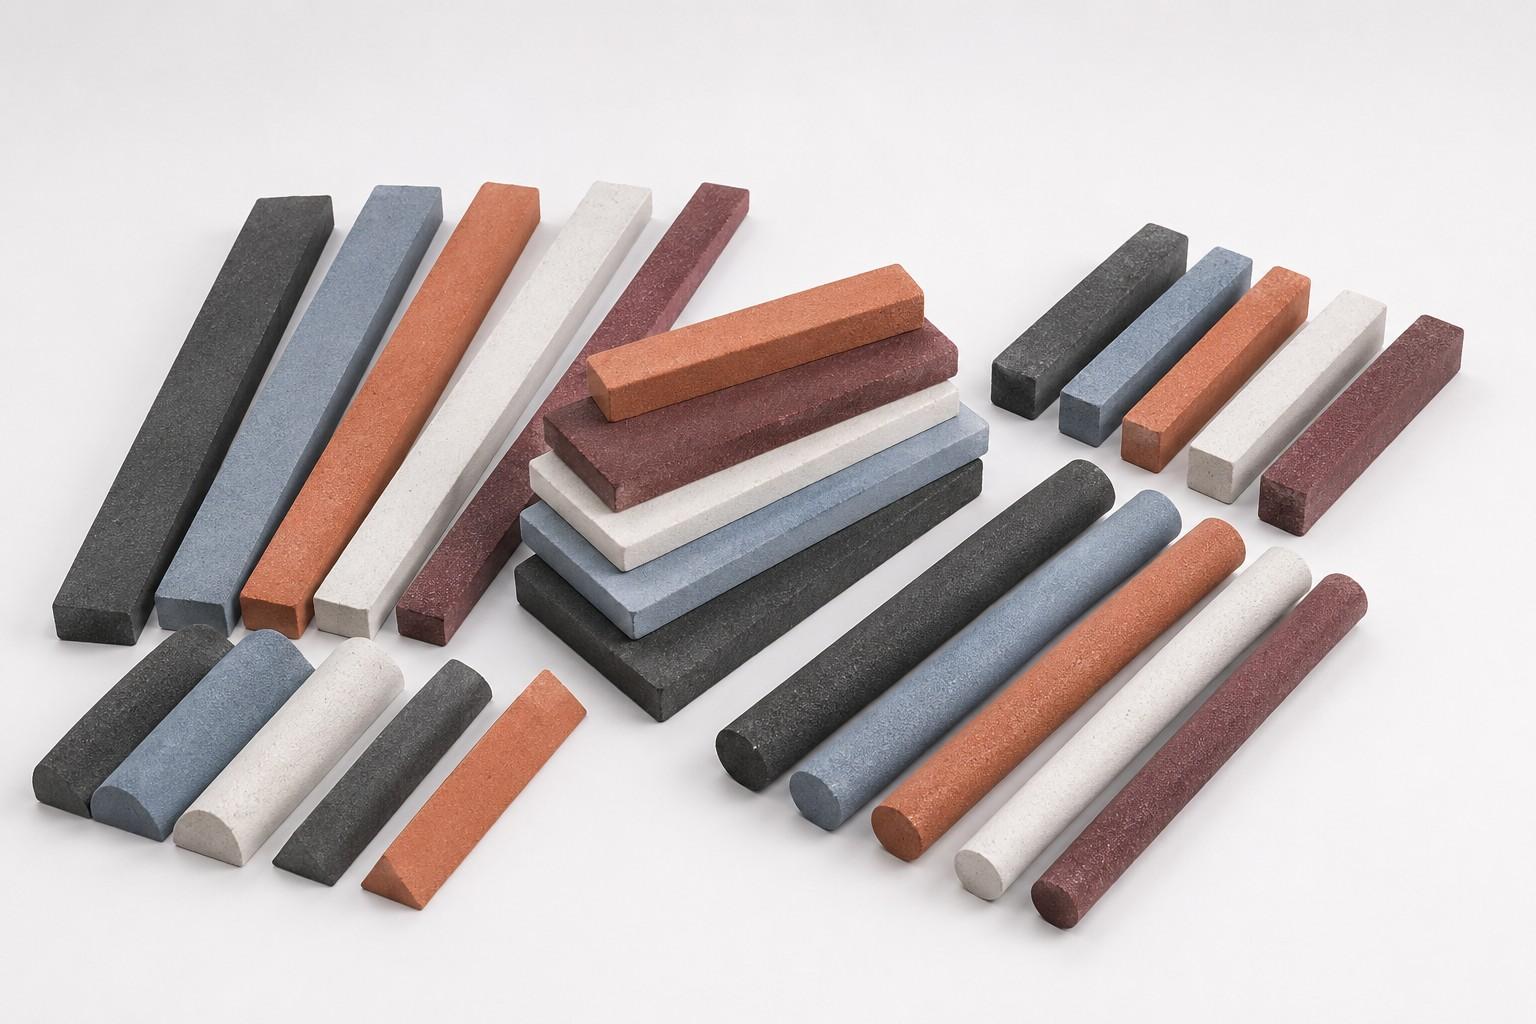
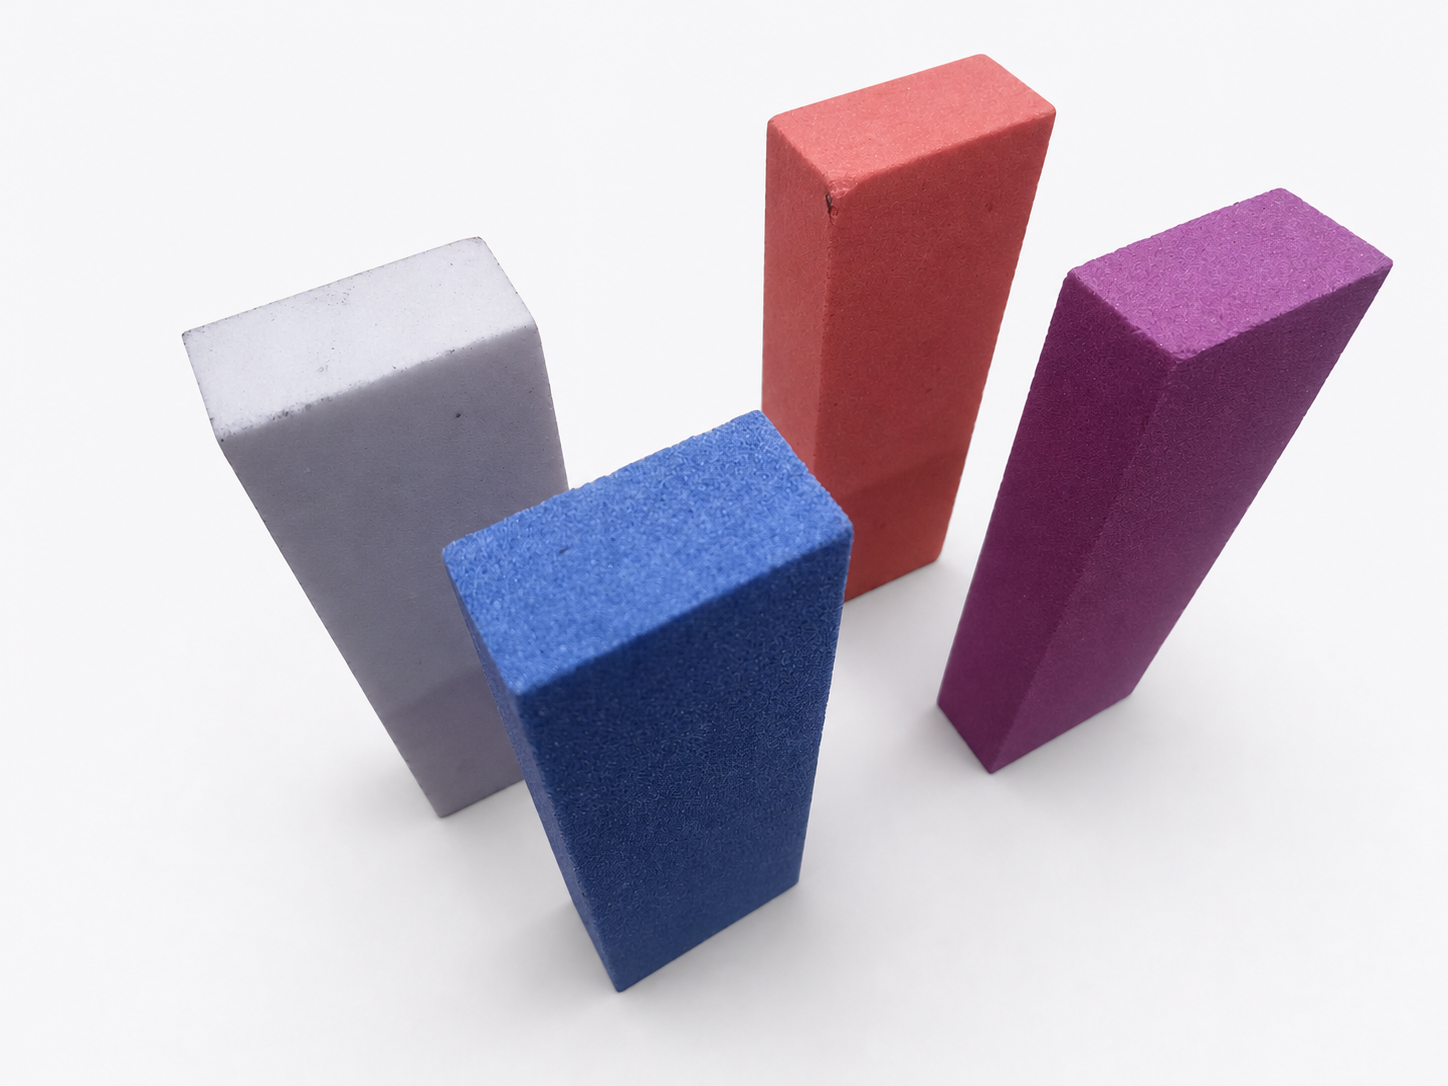
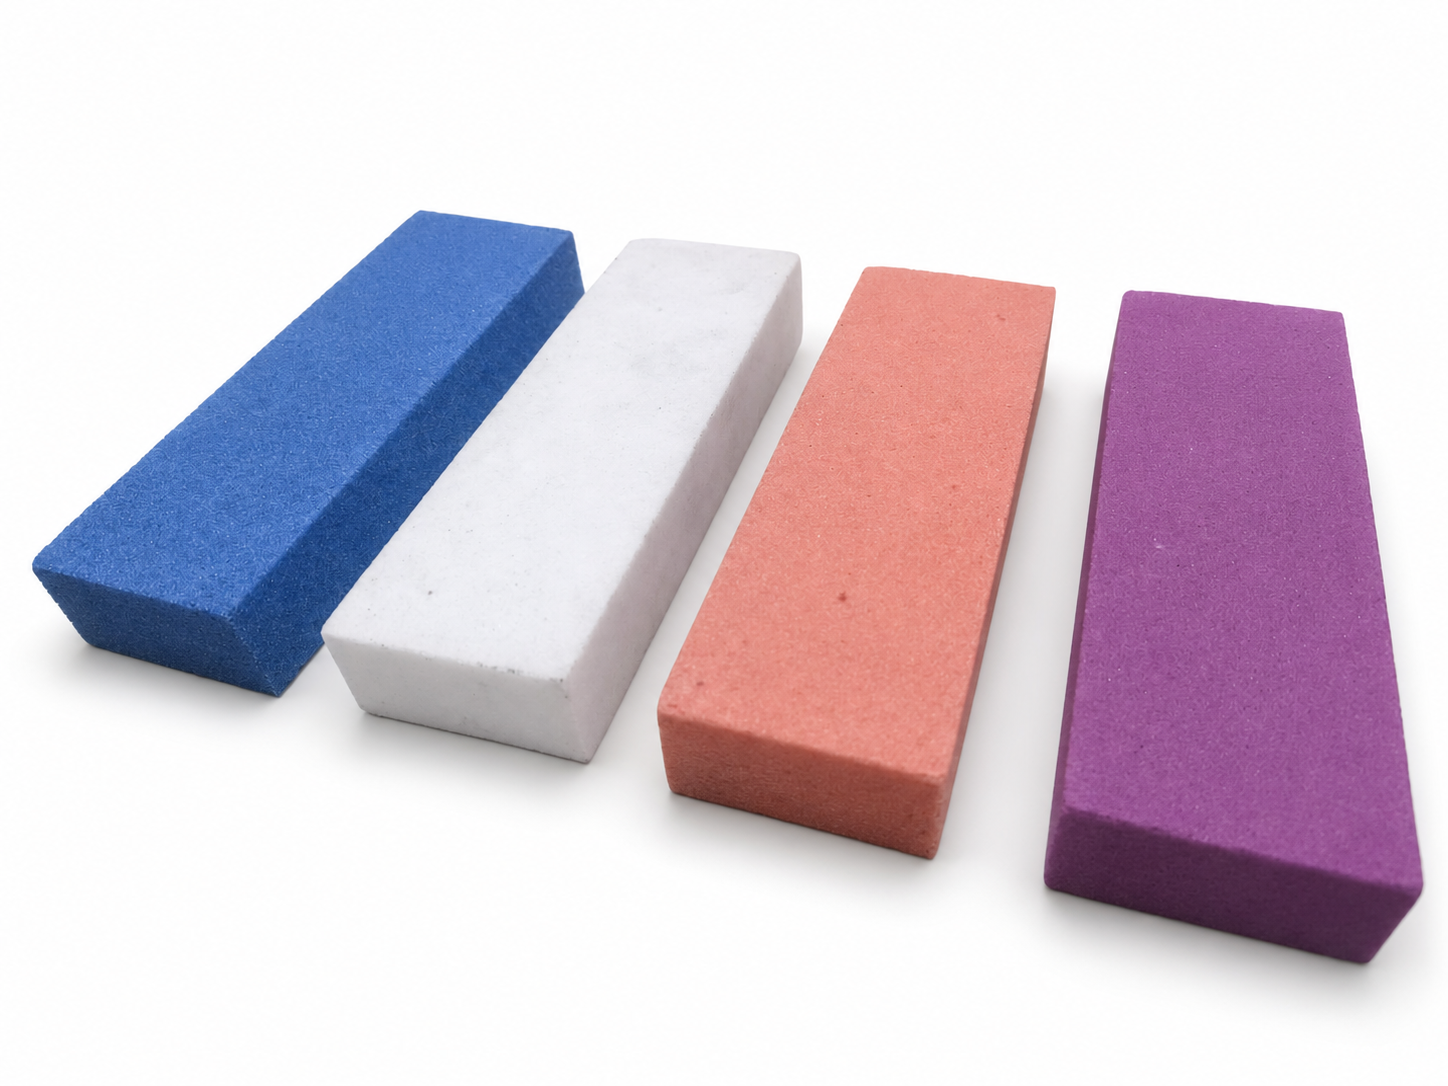
Hand-finishing stones shown in the four form families recorded in the supplied customer list.
The supplied list references 100 mm and 150 mm lengths; section size, grain and availability are quoted by RFQ.
Commercial information policy
This public brochure does not publish prices. Current commercial terms are shared only against a specific product, quantity, packing and delivery requirement.
Capability matrix
Use this matrix to move from a shop-floor need to the specification details required for a useful RFQ.
| Buyer need | Product family | Specification focus | Typical use |
|---|---|---|---|
| Die grinder mounted points | Cylinder, round-nose, cone, bullet and detail profiles | Profile, body diameter, body length, shank size, grit and bond | Bore cleanup, cavity finishing, deburring, radii blending and slot cleanup |
| Foundry and fabrication stock removal | Coarse mounted points and abrasive sticks | Material, burr size, die-grinder RPM, removal rate, grit and quantity | Casting flash removal, fettling, weld dressing and edge preparation |
| Custom abrasive specifications | Mounted points, oil stones and abrasive sticks | Drawing or sample, grain, grit, grade, bond, minimum quantity and lead time | Non-standard access, repeat production references and special finishing work |
Product use domains
Each domain below shows the typical operation, matching product family and the reason that abrasive form is selected.
Operation: Cavity blending, radii finishing, slot cleanup and edge breaking
Products used: Cone, round-nose and cylindrical mounted points
Small mounted points reach shaped cavities and controlled corners without overcutting.

Operation: Casting flash removal, gate cleanup, fettling and rough burr removal
Products used: Coarse cylindrical mounted points, silicon-carbide options and abrasive sticks
Coarser abrasives remove scale, casting marks and excess metal after shakeout.

Operation: Weld seam dressing, weld-toe blending, chamfer cleanup and edge preparation
Products used: Bullet-profile points, large cylinders and abrasive sticks
The range supports detail blending, edge preparation and controlled stock removal with mounted points.

Operation: Part deburring, fixture cleanup, toolroom correction and repeat finishing
Products used: A / WA mounted points, oil stones and abrasive sticks
Repeatable grit and shape choices help maintain consistent part-edge condition.

Operation: Bench grinding, sharpening, internal touch-up and repair grinding
Products used: Oil stones, abrasive sticks, custom abrasive references and fine-detail mounted points
Daily maintenance teams need quick access to standard sizes and predictable finishing behavior.

Operation: Small bore finishing, miniature slot cleanup, jewelry and dental lab finishing
Products used: Fine cylinders, mini round-nose profiles and other 3 mm shank mounted points
Small shank mounted points allow controlled finishing in restricted-access work.

Selection guide

Abrasive codes
General steel grinding and deburring
Cooler cutting and sharper finish on hardened steels
Controlled finishing where grain sharpness matters
Cast iron, non-ferrous and brittle material applications
Quality process
Featured references
Cylinder profile
Typical body: ⌀3-10 × 6-20 mm
Large cylinder profile
Typical body: ⌀20-25 × 20-50 mm
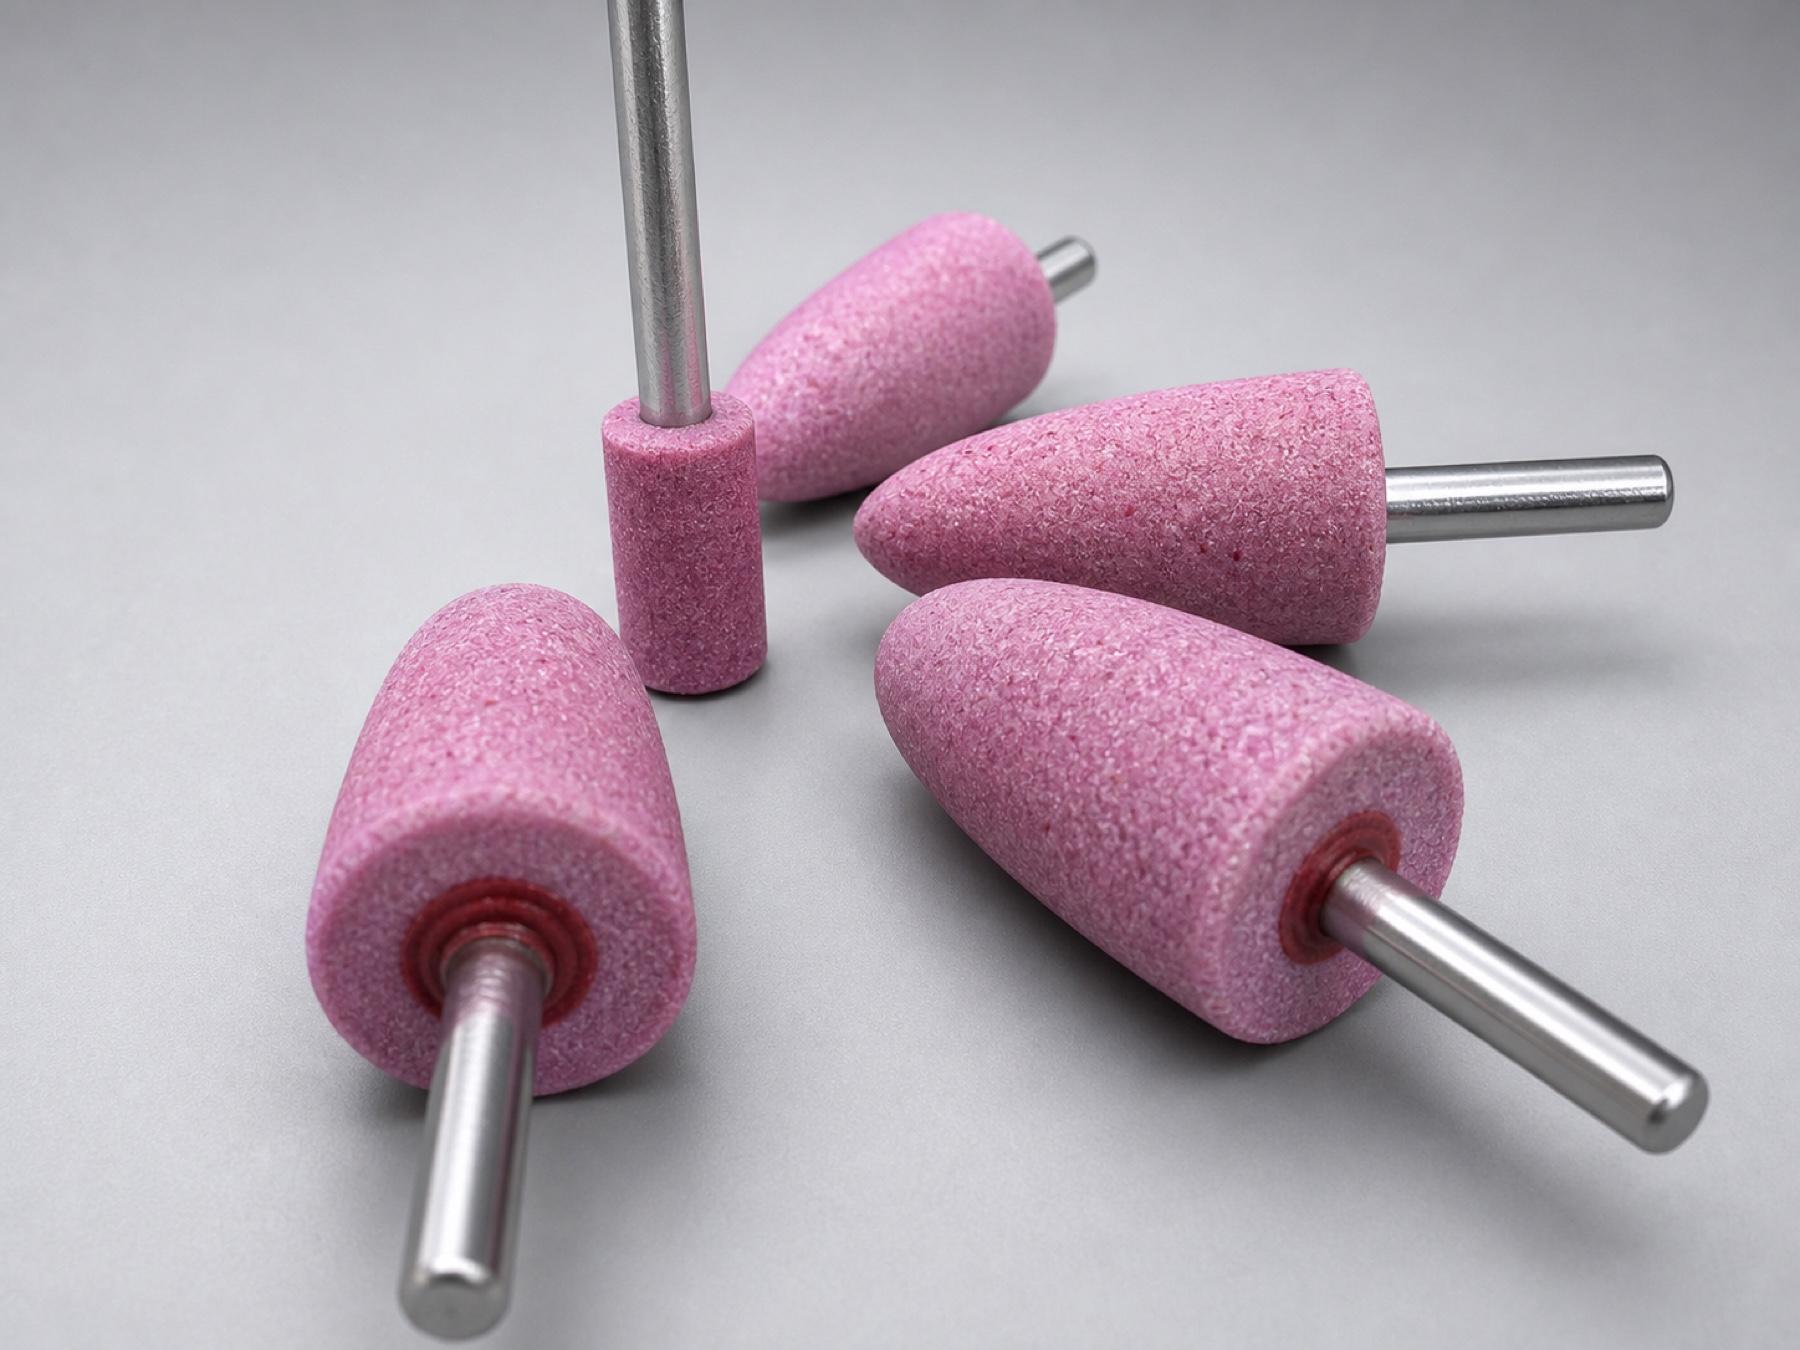
Round-nose profile
Typical body: ⌀3-13 × 10-25 mm
Contour profile
Typical body: ⌀10-22 × 20-50 mm
Bullet profile
Typical body: ⌀10-16 × 16-25 mm
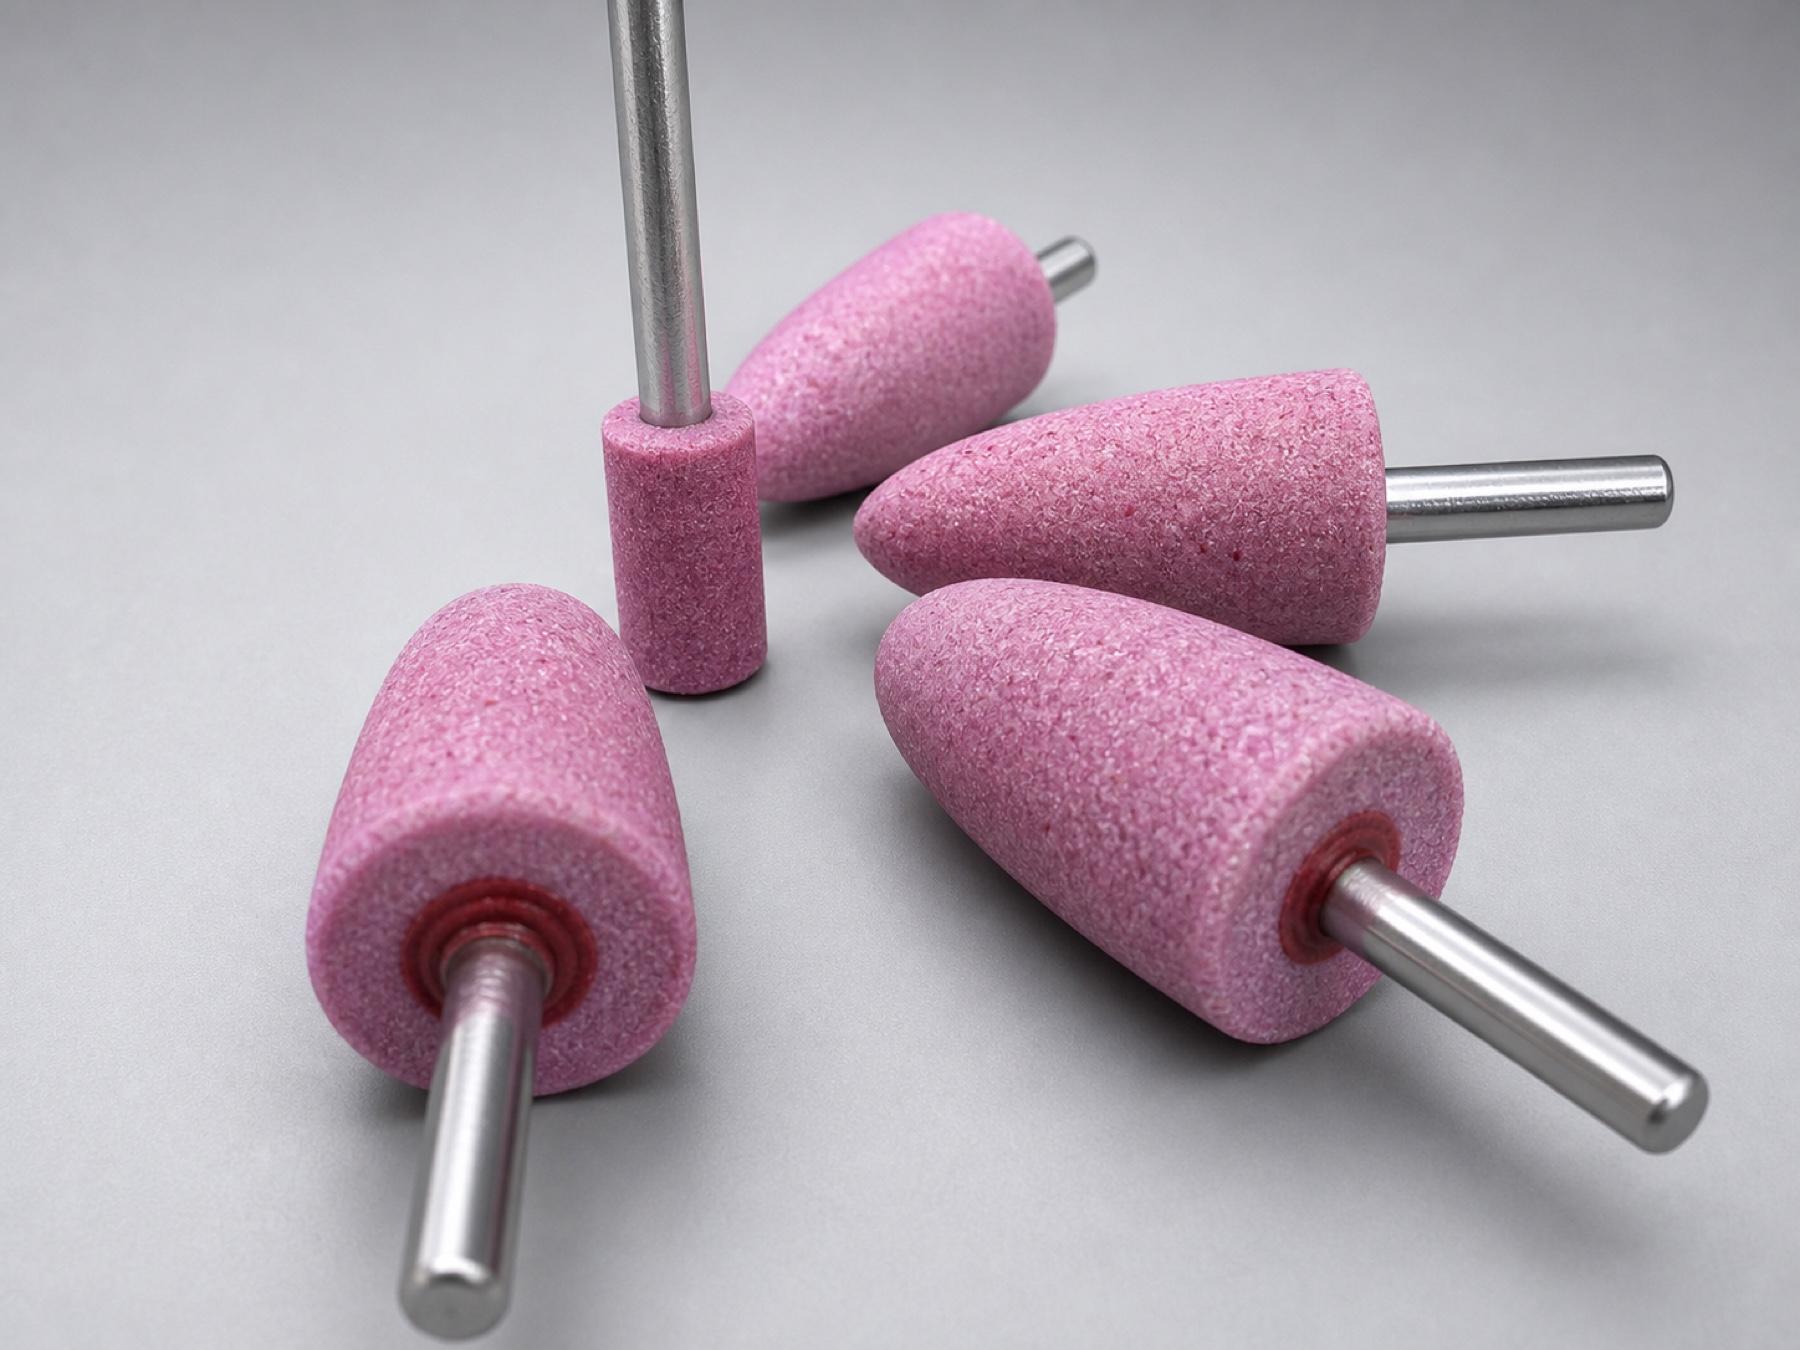
Fine cylinder profile
Typical body: ⌀3-6 × 3-13 mm
Professional selection path
A reliable abrasive enquiry starts with the operation and machine, then moves to abrasive shape and mounted-point geometry, abrasive grain, grit, grade, bond, safe-speed confirmation and quantity. This makes repeat orders easier and reduces back-and-forth for purchasing teams.
Confirm material, machine, access area, removal target and finish expectation.
Select shape, abrasive grain, grit, grade, bond, shank and safe-speed reference.
Confirm quantity, packing, dispatch preference and any repeat-order reference.
Use accepted quotation and product marking for repeatable future enquiries.
Safety and fit checks
Confirm machine RPM against product marking before use.
Use the correct guard, flange, shank overhang and mounting method.
Inspect every abrasive for cracks, damage or poor fit before mounting.
Use eye, face, hand and respiratory protection suitable for the operation.
Product tables
Dimensions and safe speed must be confirmed against the machine, guard and work material before use.
Mounted abrasive profiles on steel shanks for compatible die grinders and flexible-shaft machines.
| Profile | Product | Size | Abrasive / grit | Bond / speed | Primary use |
|---|---|---|---|---|---|
| Cylinder profile | Mounted Point - Compact Cylinder | Typical body: ⌀3-10 × 6-20 mm | Aluminum Oxide (A) / White AO (WA) / 46, 60, 80, 120, 180 | Vitrified (V) / Confirm the maximum RPM on the quoted product marking; permitted speed changes with shank diameter and unsupported overhang. | Internal bore grinding, Deburring weld seams |
| Large cylinder profile | Mounted Point - Large Cylinder | Typical body: ⌀20-25 × 20-50 mm | Aluminum Oxide (A) / Silicon Carbide (C) / 24, 36, 46, 60, 80 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Heavy stock removal, Face grinding |
| Long cylinder profile | Mounted Point - Long Cylinder | Typical body: ⌀10-20 × 25-40 mm | Aluminum Oxide (A) / 46, 60, 80, 120 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | General grinding, Tool room work |
| Round-nose profile | Mounted Point - Round-Nose Cylinder | Typical body: ⌀3-13 × 10-25 mm | Aluminum Oxide (A) / Pink AO (PA) / 60, 80, 120, 180 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Contour blending, Die polishing |
| Contour profile | Mounted Point - Contour Profile | Typical body: ⌀10-22 × 20-50 mm | Aluminum Oxide (A) / Silicon Carbide (C) / 46, 60, 80, 120 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Edge grinding, Deburring |
| Bullet profile | Mounted Point - Bullet Profile | Typical body: ⌀10-16 × 16-25 mm | Aluminum Oxide (A) / 46, 60, 80, 120 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Weld toe blending, Fillet radius dressing |
| Cone profile | Mounted Point - Cone Profile | Typical body: ⌀6-10 × 20-32 mm | Aluminum Oxide (A) / 46, 60, 80 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Chamfer grinding, Seat and chamfer touch-up |
| Fine cylinder profile | Mounted Point - Fine Cylinder | Typical body: ⌀3-6 × 3-13 mm | Aluminum Oxide (A) / White AO (WA) / 120, 180, 220, 320 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Restricted-access finishing, Fine deburring |
| Slim cylinder profile | Mounted Point - Slim Detail Cylinder | Typical body: ⌀3-6 × 8-16 mm | White Aluminum Oxide (WA) / Pink AO (PA) / 120, 180, 220, 320 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Miniature die finishing, Small slot deburring |
| Heavy long cylinder profile | Mounted Point - Heavy Long Cylinder | Typical body: ⌀20-25 × 32-50 mm | Aluminum Oxide (A) / Silicon Carbide (C) / 24, 36, 46, 60 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Casting flash removal, Weld dressing |
| Mini round-nose profile | Mounted Point - Mini Round-Nose | Typical body: ⌀3-8 × 10-20 mm | White Aluminum Oxide (WA) / Pink AO (PA) / 120, 180, 220, 320 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Small radius blending, Fine mold cavity finishing |
| Slim cone profile | Mounted Point - Slim Cone | Typical body: ⌀6-10 × 20-32 mm | Aluminum Oxide (A) / Silicon Carbide (C) / 46, 60, 80, 120 | Vitrified (V) / Confirm maximum RPM from the quoted product marking and permitted shank overhang before use. | Counter-sink finishing, Chamfer deburring |
Profiles and dimensions are enquiry references. Final dimensions, shank, bond and rated speed are controlled by the accepted quotation, approved drawing and product marking.

RFQ checklist
Contact
Mounted point manufacture and abrasive RFQ support
Email: info@sadhviudyog.com
Phone: +91 87916 94259
Address: 124, New Shiv Puri, Behind J.P. Public School, Aara Mill, Khurja - 203131, Uttar Pradesh, India
GST: 09APXPM7548B1ZA
Hours: Mon-Sat, 9 AM - 6 PM IST
Order and supply process
This brochure describes the buyer-facing order flow: application fit, abrasive selection, geometry confirmation and dispatch communication.
Step 1
The buyer shares the required shape, dimensions, work material, machine RPM and finish target so the enquiry can be tied to the actual job.
Step 2
Abrasive grain, grit size, grade and bond are reviewed against stock removal, finish expectation and operating conditions before quotation.
Step 3
The accepted quotation records the agreed product geometry, shank requirement and intended use before supply moves forward.
Step 4
Applicable dimensions, identification, rated-speed information and packing details are confirmed for dispatch and future repeat-order reference.
Buyer trust
Trust comes from repeatable process, visible checkpoints and better specification control, not from broad claims alone.
The order is not treated as a generic abrasive item. Profile, size, grit, bond and application are confirmed before supply moves forward.
Applicable dimensional checks, identification, safe-speed information and packing requirements can be recorded in the accepted quotation.
Sharing the previous quotation, product marking and application notes makes a repeat enquiry clearer than relying on appearance alone.
The site, brochure and RFQ flow are built around die shops, foundries, fabrication units, toolrooms and component manufacturers, not generic retail messaging.
Catalogue principles
Separate mounted points, oil stones, abrasive sticks and custom specifications so buyers can reach the right technical table quickly.
Describe the operation in shop-floor terms such as deburring, fettling, bore cleanup, tool grinding and surface finishing.
Show shape, size, grain, grit, bond and machine details so purchasing and production teams can compare options.
Guide selection by work material, access area, machine type, finish requirement and expected stock removal.
Keep speed, guard and mounting checks visible because final safe use depends on the tool, machine and operating setup.


